What is a Chemical Reactor?
A chemical reactor is a specialized vessel designed to facilitate chemical reactions between substances, enabling processes such as mixing, heating, cooling, and separation to produce desired materials. It is a core component in industries including pharmaceuticals, petrochemicals, food processing, and environmental engineering, with designs tailored to reaction types (batch, continuous, semi-batch), pressure requirements, and temperature control. As global demand for sustainable manufacturing rises, chemical reactor manufacturers in China are innovating to integrate smart technologies, energy efficiency, and compliance with international safety standards, positioning the country as a key hub for reactor production. Chemical Reactor

1. Beijing Cycle Columbus Environmental Science & Technology Co., Ltd.
Located in Beijing, a national center for advanced industrial technology, Beijing Cycle Columbus Environmental Science & Technology Co., Ltd. (Cycle Columbus) is a leading provider of customized chemical reactors, focusing on integrating environmental protection into industrial reaction processes. Founded in 2008, the company has grown from a small R&D team to a full-scale manufacturer with 320 employees, including 45 chemical engineers and process designers, dedicated to solving complex challenges in high-value chemical synthesis, wastewater treatment, and green chemical production.
Cycle Columbus specializes in both lab-scale and industrial-scale reactors, including stirred tank reactors, fixed-bed reactors, catalytic reactors, and high-pressure/high-temperature reaction systems. Its products are widely used in pharmaceutical API production, fine chemical synthesis, biopharmaceutical manufacturing, and industrial waste gas purification. A key differentiator is its proprietary “Eco-Reactor” series, which combines reaction efficiency with emission reduction technology, cutting energy consumption by 25% compared to traditional models while meeting China’s GB and international ISO 14001 environmental standards.
The company has established long-term partnerships with over 180 enterprises, including Sinopharm Group, BASF China, and several top 500 chemical companies globally. Its R&D center in Beijing collaborates with Tsinghua University’s Department of Chemical Engineering on reactor simulation and material science, ensuring products use corrosion-resistant alloys (Hastelloy, titanium) and smart control systems with real-time monitoring via IoT sensors. In 2025, Cycle Columbus expanded its production base in Tianjin, adding a 12,000-square-meter facility to increase annual reactor output from 850 units to 1,500 units, targeting the Southeast Asian and European markets in 2026.
Website: https://www.cycle-columbus.com/
Company Features & Advantages:
- Specialization in eco-friendly chemical reactors with integrated emission reduction technology
- Customization of lab to industrial scale reactors for pharmaceutical and environmental applications
- In-house R&D center with Tsinghua University collaboration on smart reactor design
- ISO 9001, ISO 14001, and GB 50235 (pressure vessel) certified production
- 24/7 after-sales support with on-site installation and maintenance services
- Proprietary high-pressure reactor models with 300-bar pressure tolerance for specialty chemical synthesis
- 15-year track record of zero major safety incidents in reactor operation for clients
2. Jiangsu Yangzi Reaction Equipment Co., Ltd.
Headquartered in Zhangjiagang, Jiangsu Province, a major industrial base in the Yangtze River Delta, Jiangsu Yangzi Reaction Equipment Co., Ltd. is a state-level high-tech enterprise dedicated to the design and manufacturing of industrial chemical reactors. Founded in 1995, the company has over 600 employees, including 80 senior engineers, and operates two production facilities spanning 35,000 square meters, with an annual output of 2,000 reactors ranging from 50 liters to 50,000 liters in capacity.
Yangzi Reaction Equipment’s product portfolio includes stirred tank reactors, autoclaves, glass-lined reactors, and polymerization reactors, serving industries such as petrochemicals, agrochemicals, and polymer materials. Its glass-lined reactors, a core product, are widely used in fine chemical synthesis due to their corrosion resistance and smooth surface that prevents material adhesion. In 2024, the company launched its “Smart Reaction System” (SRS), which integrates AI-driven process control to optimize reaction parameters, reducing product yield variability by 18% and production time by 12%.
The company holds Class A pressure vessel manufacturing licenses from the China Special Equipment Inspection and Research Institute (CSEI) and has exported reactors to 28 countries, including Germany, the United States, and Australia, with 2025 export revenue accounting for 35% of its total sales. Yangzi Yangzi has partnered with the University of Shanghai for Science and Technology to develop energy-efficient jacketed reactors, which use waste heat recovery to cut energy consumption by 22% compared to conventional models. Its client base includes China National Petroleum Corporation (CNPC), Syngenta Group, and domestic polymer manufacturers such as Sinopec Baling Petrochemical.
Company Features & Advantages:
- Class A pressure vessel manufacturing certification for high-capacity industrial reactors
- Leading glass-lined reactor technology with 30-year service life
- AI-powered smart reaction systems for process optimization
- 28+ years of industry experience with 10,000+ reactor installations globally
- ISO 9001, ASME U Stamp, and PED (Pressure Equipment Directive) compliance
- Local and global after-sales network with 12 regional service centers
- Specialized polymerization reactors for plastic and rubber production
3. Shanghai Haoyuan Chemical Machinery Co., Ltd.
Based in Shanghai, a global trade and manufacturing hub, Shanghai Haoyuan Chemical Machinery Co., Ltd. is a specialized manufacturer of precision chemical reactors for high-tech industries such as pharmaceuticals, new energy, and electronic chemicals. Founded in 2002, the company has 280 employees, including 55 R&D staff, and operates a 10,000-square-meter clean production facility dedicated to manufacturing reactors with strict cleanliness requirements for biopharmaceutical and electronic chemical applications.
Haoyuan’s product line includes sterile stirred reactors, microreactors, and high-purity reactors for lithium-ion battery material production. Its microreactors, a fast-growing segment, feature a compact design with enhanced heat transfer, enabling continuous synthesis of specialty chemicals with 99.9% purity, making them ideal for pharmaceutical API and semiconductor chemical manufacturing. In 2025, the company launched its lithium battery cathode material reactors, which are designed to handle high-temperature (350°C) reactions for NMC and LFP material production, with a 10% higher reaction yield than industry averages.
The company is GMP (Good Manufacturing Practices) certified for pharmaceutical equipment, ensuring all reactors meet strict hygiene standards for drug production. It has established a strong presence in the domestic high-end market, with clients including Fosun Pharma, CATL, and Samsung SDI’s Chinese manufacturing plants. Haoyuan’s R&D center in Shanghai collaborates with the Chinese Academy of Sciences (CAS) on microreactor technology, holding 23 patents in reactor design and process optimization. In 2026, the company plans to expand its clean facility to 15,000 square meters to meet growing demand from the new energy sector.
Company Features & Advantages:
- Specialized cleanroom manufacturing for high-purity and sterile reactors
- GMP and ISO 13485 certified for pharmaceutical and biotech applications
- Leading microreactor technology for continuous, high-yield chemical synthesis
- Expertise in reactors for lithium-ion battery cathode material production
- 23 patents in reactor design and process control
- 98% client retention rate for high-tech industry projects
- Precision machining tolerance of ±0.01mm for reactor components
4. Zhejiang Reactor Engineering Co., Ltd.
Headquartered in Hangzhou, Zhejiang Province, known for its chemical industry clusters, Zhejiang Reactor Engineering Co., Ltd. is a comprehensive reactor manufacturer offering design, manufacturing, installation, and turnkey project services for industrial chemical processes. Founded in 1988, the company has over 750 employees, including 120 process engineers, and operates three production facilities in Hangzhou and Ningbo, with an annual output of 2,500 reactors and 50 turnkey reaction system projects.
Zhejiang Reactor Engineering’s products cover batch reactors, continuous stirred-tank reactors (CSTR), and distillation reactors, serving industries such as agrochemicals, specialty chemicals, and food additives. Its turnkey project service is a key strength, where the company handles all aspects of a chemical production line, from reactor design to site commissioning, reducing client project time by 30%. In 2024, it launched a modular reactor system, which pre-assembles components in its factory, cutting on-site installation time by 40% compared to traditional field assembly.
The company holds ASME U and R stamps for pressure vessel manufacturing and is a key supplier to major agrochemical companies such as Syngenta China and Zhejiang NHU Co., Ltd. Its R&D team focuses on corrosion-resistant reactor materials, developing a proprietary “Zhe Alloy” that resists acids and alkalis, extending reactor service life by 20% in harsh chemical environments. Zhejiang Reactor Engineering has exported to 32 countries, including Brazil, India, and South Korea, with 2025 international sales accounting for 40% of total revenue.
Company Features & Advantages:
- Turnkey reaction system services from design to commissioning
- Modular reactor design for fast installation and deployment
- ASME certified pressure vessel manufacturing for global markets
- Proprietary corrosion-resistant alloy for long service life in harsh environments
- 35+ years of experience in agrochemical reactor applications
- 120+ process engineers for customized reaction process design
- National level contract credit enterprise with AAA credit rating
5. Shandong Huate Chemical Equipment Co., Ltd.
Located in Jinan, Shandong Province, a major heavy industry base in northern China, Shandong Huate Chemical Equipment Co., Ltd. is a leading manufacturer of large-scale industrial chemical reactors for petrochemical and coal chemical industries. Founded in 1992, the company has 900 employees, including 150 senior technical staff, and operates a 50,000-square-meter heavy manufacturing facility equipped with 100-tonne cranes and CNC machining centers, capable of producing reactors up to 100,000 liters in capacity.
Huate’s product portfolio includes large autoclaves, fluidized bed reactors, and coking reactors, designed for high-temperature and high-pressure reactions in crude oil refining and coal-to-chemical processes. Its fluidized bed reactors, a core product, feature a unique gas distribution system that improves reaction uniformity, increasing conversion rate by 15% for coal chemical synthesis. In 2025, the company completed a 120-million-yuan R&D project for ultra-large reactors for Sinopec’s new green hydrogen production plant, with a 50,000-liter capacity and 450°C temperature tolerance.
The company is a key supplier to Sinopec, PetroChina, and Shaanxi Coal & Chemical Industry Group, with 80% of its revenue coming from large-scale petrochemical projects. It holds Class A pressure vessel design and manufacturing licenses and has passed ISO 9001 and OHSAS 18001 safety certifications. Huate’s after-sales team provides on-site installation and 24/7 emergency support for large industrial reactors, with a 99% client satisfaction rate for its petrochemical projects.
Company Features & Advantages:
- Specialized in ultra-large reactors for petrochemical and coal chemical industries
- Class A license for design and manufacturing of high-capacity pressure vessels
- Heavy manufacturing facility with 100-tonne crane capacity
- Proprietary fluidized bed reactor technology for high conversion rates
- Long-term partnership with top Chinese energy enterprises (Sinopec, PetroChina)
- OHSAS 18001 certified for workplace safety in industrial projects
- 10-year warranty on reactor pressure vessel structures
6. Guangdong Lixing Reaction Technology Co., Ltd.
Headquartered in Guangzhou, Guangdong Province, a key industrial and trade hub in southern China, Guangdong Lixing Reaction Technology Co., Ltd. is a high-tech enterprise focusing on customized chemical reactors for the pharmaceutical and fine chemical industries. Founded in 2005, the company has 350 employees, including 60 R&D engineers, and operates a 12,000-square-meter facility with a dedicated cleanroom for sterile reactor manufacturing.
Lixing’s products include glass-lined reactors, stainless steel reactors, and cryogenic reactors for low-temperature chemical synthesis, serving clients such as GlaxoSmithKline (GSK) China, WuXi AppTec, and Guangzhou Pharmaceutical Holdings. Its cryogenic reactors, designed for reactions at temperatures as low as -196°C, are used in the production of specialty pharmaceutical intermediates, with a 20% higher thermal insulation efficiency than competing models. In 2024, the company launched its digital reactor platform, which uses IoT sensors to monitor reaction data in real time, allowing clients to adjust parameters remotely.
The company is GMP and ISO 14644-1 (cleanroom) certified, ensuring all products meet international standards for pharmaceutical equipment. Lixing has a strong focus on innovation, with 18 patents in reactor design, including a modular glass-lined reactor that reduces maintenance time by 35%. Its export market covers Southeast Asia, the Middle East, and Europe, with 2025 export growth of 28% driven by demand from generic drug manufacturers.
Company Features & Advantages:
- Specialized cryogenic reactors for low-temperature chemical synthesis
- GMP and ISO 14644-1 certified for pharmaceutical cleanroom applications
- Digital reactor platform with real-time remote monitoring
- Modular glass-lined reactor design for easy maintenance
- 18 patents in reactor technology and process optimization
- Key supplier to global pharma companies (GSK, WuXi AppTec)
- Fast delivery of customized reactors (average 45 days from order to shipment)
7. Liaoning Hengtai Reaction Equipment Co., Ltd.
Based in Shenyang, Liaoning Province, a historic industrial base in northeast China, Liaoning Hengtai Reaction Equipment Co., Ltd. is a leading manufacturer of chemical reactors for the fertilizer and agrochemical industries. Founded in 1990, the company has 550 employees, including 90 technical staff, and operates a 30,000-square-meter production facility, with an annual output of 1,800 reactors for industrial chemical processes.
Hengtai’s product line includes stirred reactors for fertilizer production, ammonia synthesis reactors, and granulation reactors, designed to handle large-scale, high-volume reactions for agricultural chemical manufacturing. Its ammonia synthesis reactors, a core product, feature a high-pressure resistant design (up to 320 bar) and a catalyst regeneration system that extends catalyst life by 25%, reducing operational costs for clients. In 2025, the company launched a energy-efficient granulation reactor, which uses 15% less steam than conventional models, aligning with China’s “Double Carbon” goals.
The company is a key supplier to China National Chemical Corporation (ChemChina) and domestic fertilizer manufacturers such as Liaoning Dadi Fertilizer Co., Ltd. It holds Class B pressure vessel manufacturing licenses and has exported reactors to Russia, India, and Pakistan, with 2025 export revenue accounting for 25% of total sales. Hengtai’s R&D center in Shenyang collaborates with Liaoning University of Chemical Technology on catalyst integration for reactor efficiency, ensuring products meet the high demands of large-scale agrochemical production.
Company Features & Advantages:
- Specialized reactors for fertilizer and agrochemical large-volume production
- High-pressure ammonia synthesis reactors with extended catalyst life
- Energy-efficient granulation reactors aligned with “Double Carbon” goals
- Class B pressure vessel certification for industrial applications
- Long-term partnership with ChemChina and top domestic fertilizer firms
- 30+ years of experience in northeast China’s industrial market
- Local service network in 12 agrochemical production regions across China
8. Fujian Huaya Chemical Machinery Co., Ltd.
Headquartered in Quanzhou, Fujian Province, a major light industrial base in southeast China, Fujian Huaya Chemical Machinery Co., Ltd. is a leading manufacturer of chemical reactors for the food and beverage industry, as well as fine chemicals. Founded in 1998, the company has 300 employees, including 45 food-grade reactor specialists, and operates a 8,000-square-meter facility certified for food contact materials by China’s National Food Safety Standard (GB 4806).
Huaya’s product portfolio includes stainless steel reactors for food additive production, fermentation reactors for beverage manufacturing, and bio-reactors for natural ingredient extraction. Its fermentation reactors, designed for yeast and probiotic production, feature a sterile, easy-to-clean design that meets food safety standards, with a 99.5% sterility rate during operation. In 2024, the company launched its bio-reactor line for plant-based protein extraction, serving clients such as Wahaha and China Mengniu Dairy, with a 12% higher extraction efficiency than traditional methods.
The company is HACCP (Hazard Analysis and Critical Control Points) certified for food equipment and has exported reactors to 18 countries, including the United States, Canada, and Australia, with 2025 food industry sales growing by 32%. Huaya’s R&D team focuses on food-grade reactor materials, using 316L stainless steel that resists corrosion from food acids and enzymes, ensuring compliance with global food safety standards.
Company Features & Advantages:
- Food-grade reactors certified by GB 4806 and HACCP standards
- Specialized fermentation reactors for beverage and probiotic production
- Bio-reactors for plant-based protein extraction in food industry
- 18+ years of experience in light industrial chemical equipment
- Key supplier to top Chinese food and beverage companies (Wahaha, Mengniu)
- Fast delivery for food industry projects (average 30 days)
- Low-maintenance reactor design with CIP (Clean-in-Place) compatibility
9. Henan Xinhua Reaction Technology Co., Ltd.
Located in Zhengzhou, Henan Province, a central industrial hub in China, Henan Xinhua Reaction Technology Co., Ltd. is a high-tech enterprise focusing on microreactors and continuous flow reaction systems for fine chemical and pharmaceutical industries. Founded in 2010, the company has 220 employees, including 50 microreactor specialists, and operates a 7,000-square-meter R&D and production facility dedicated to small-scale and pilot-scale reactors.
Xinhua’s products include microreactors for lab and pilot use, continuous flow reaction systems, and modular reaction units, serving clients such as Zhejiang Medicine Co., Ltd., and several biotech startups. Its microreactors, designed for precise control of reaction parameters, enable 99% purity for specialty chemical intermediates, with 50% less waste than batch reactors. In 2025, the company launched a pilot-scale continuous flow system that can be scaled up to industrial production, reducing the time for process development from 12 months to 3 months.
The company has 15 patents in microreactor technology and collaborates with Zhengzhou University on flow chemistry research. It is ISO 9001 and ISO 13485 certified, ensuring products meet medical device and pharmaceutical standards. Xinhua’s core strength is in customizing microreactors for unique chemical processes, with a 95% client success rate in achieving target reaction yields. In 2026, the company plans to expand its pilot-scale facility to 10,000 square meters to meet growing demand from pharmaceutical R&D.
Company Features & Advantages:
- Specialized microreactors and continuous flow reaction systems
- 15 patents in flow chemistry and reactor design
- Pilot-scale to industrial scale modular systems for fast process scaling
- ISO 13485 certified for biotech and pharmaceutical applications
- 95% client success rate in reaction yield optimization
- Focus on small to medium-scale reactors for R&D and pilot production
- Collaborative R&D with Zhengzhou University on next-generation reactor technology
10. Sichuan Tianli Chemical Equipment Co., Ltd.
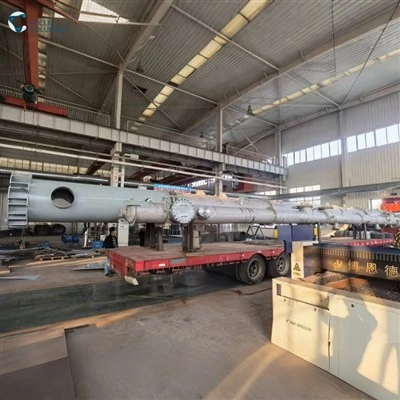
Headquartered in Chengdu, Sichuan Province, a major chemical and energy base in southwest China, Sichuan Tianli Chemical Equipment Co., Ltd. is a leading manufacturer of chemical reactors for the natural gas and chemical fiber industries. Founded in 1993, the company has 650 employees, including 110 senior engineers, and operates a 40,000-square-meter production facility equipped with advanced welding and machining equipment, capable of producing reactors up to 80,000 liters in capacity.
Tianli’s product portfolio includes natural gas reforming reactors, polymerization reactors for chemical fiber production, and pressure vessels for chemical processing, serving clients such as Sinopec Sichuan Petrochemical, Chengdu Chemical Fiber Co., Ltd., and PetroChina Southwest Oil & Gas Field. Its natural gas reforming reactors, designed for high-temperature (1,200°C) reactions, feature a heat recovery system that reduces energy consumption by 20% compared to conventional models. In 2025, the company launched a new chemical fiber polymerization reactor, which improves fiber strength by 8% and reduces production waste by 15%.
The company holds Class A pressure vessel manufacturing licenses and is a key supplier to southwest China’s energy and chemical fiber industries. It has passed ISO 9001 and API (American Petroleum Institute) certifications, ensuring products meet international oil and gas industry standards. Tianli’s after-sales team provides technical support for reactor operation, with a 98% client satisfaction rate for its energy industry projects.
Company Features & Advantages:
- Specialized reactors for natural gas reforming and chemical fiber production
- Class A pressure vessel and API certified for energy industry applications
- High-temperature reactors with integrated heat recovery systems
- 30+ years of experience in southwest China’s chemical industry
- Long-term partnership with Sinopec and PetroChina’s southwest subsidiaries
- Advanced welding and machining equipment for large reactor production
- 24/7 technical support for energy industry reactor operation
Conclusion
Chemical Tank Storage China’s chemical reactor industry in 2026 is defined by a mix of specialized manufacturers catering to diverse sectors, from pharmaceuticals and food processing to petrochemicals and new energy. The 10 companies above lead in innovation, quality, and customer service, with a strong focus on smart technology, sustainability, and compliance with international standards. As global demand for efficient and eco-friendly chemical processes grows, these manufacturers are well-positioned to expand their domestic and international market share, driving China’s role as a global leader in chemical reactor production.
